The AK-47 · Volume 24
Verification — What Is Established, and What Is Still Assumed
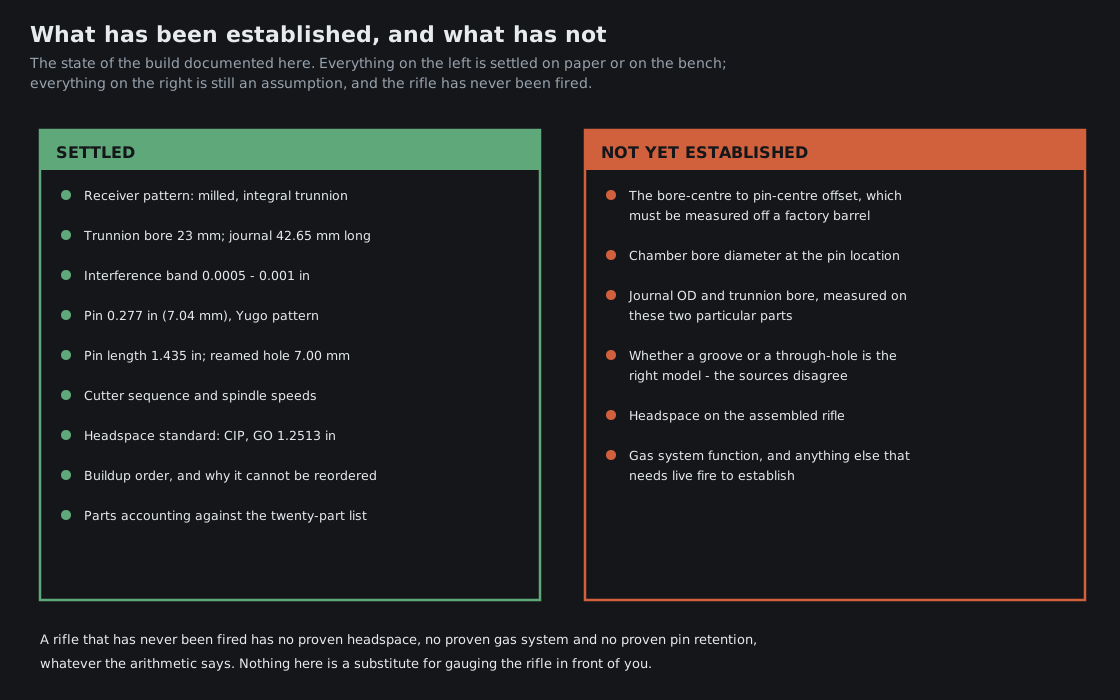
The honest summary of this build arm is short: nothing in Vols 17 to 23 has been proved on a rifle, because the rifle has never been fired. The specifications are recorded, the procedures are worked out, the arithmetic has been done and checked — and three measurements that the work depends on have not been taken. This volume separates the two categories, because a set of volumes this specific can read as more finished than it is.
24.1 Settled
The legal frame and the parts accounting. The twenty-part list at 27 CFR 478.39(c) is a closed list quoted from the regulation, and the parts selection for this rifle sits well under the ten-part limit with six or seven American parts by construction and by choice. Vol 17.
The receiver, dimensionally. Milled, integral front trunnion, M70 pattern: trunnion bore about 23 mm, journal length about 42.65 mm, interference band 0.0005–0.001 in. No cross-hole in either trunnion wall. Vol 18.
Tooling and cutter sequence. 1/4 in four-flute end mill at 800–1,200 rpm to spot; 17/64 in cobalt drill at 500–700 rpm through all three walls; 7 mm chucking reamer at 150–250 rpm in one pass. Pilot drills of 5/32 in and 1/8 in for the component pins. Vol 19.
The headspace standard, and why. CIP, not SAAMI: GO 1.2513 in must close, NO-GO at about 1.257–1.260 in must not, FIELD at about 1.264–1.270 in condemns the rifle. The reason is that the standards differ in shoulder angle as well as length, so a gauge from one standard misreads a chamber cut to the other. Vol 20.
The buildup order, and why it is forced. Rear sight base, retainer band, gas block, front sight base — in that order, all before the receiver press-in, because the band cannot pass the gas block and because the receiver blocks access afterwards. Vol 21.
The pin specification. 0.277 in (7.04 mm) diameter, 1.435 in long, into a 7.00 mm reamed hole with 0.001–0.0015 in of interference; pressed, never hammered; oversize 0.302 in available as the one recovery path. Vol 22.
The joint model. A 7.04 mm through-hole cannot fit in the 6.36 mm of wall available below the chamber bore, so the joint is a groove spanned by the pin rather than a hole through the journal. Vol 23, where the arithmetic is worked.
The groove analysis, conditionally. 3.5 mm deep, 7.0 mm wide, semi-circular, cut with a 7 mm ball end mill to 32 Ra — with the burst, bearing and fatigue reasoning behind each number, and with the two internal inconsistencies in the source analysis identified and corrected. Vol 23.
24.2 Not Established
The bore-centre to pin-centre offset. This is the gating item. It is a design dimension of the barrel pattern that cannot be calculated from the receiver, and the way to obtain it is to measure a factory barrel that already has its hole, in a V-block, from bore centre to pin-hole centre. It has not been measured. Without it, the operation in Vol 22 cannot begin, and the two ways of getting it wrong both destroy the barrel.
The chamber bore diameter at the groove’s position. Vol 23 uses drawing figures and works the worst case. Between the worst and best chamber stations the available wall differs by more than a millimetre, which is a third of the recommended groove depth.
The actual journal OD and trunnion bore. The 0.0005–0.001 in interference is a specification, not a measurement of these two parts. Both get measured before the press, and the press-in cannot responsibly start until they have been.
Headspace on this rifle. The standard is settled; the rifle has not been gauged, because the barrel has not been pressed in.
Gas system function. Port alignment has a documented check — light through the gas block port and the barrel port — and that check has not been performed on this barrel. Whether the rifle cycles is not knowable from any of it.
Everything that requires live fire. Pin retention under repeated firing, fatigue behaviour at the groove root, real headspace behaviour under pressure, and whether the rifle functions at all.
24.3 What Proving This Build Would Look Like
Stated as a sequence, because the order is as constrained as the buildup order in Vol 21:
- Measure a factory barrel of this pattern and establish the Y offset. Corroborate against a second measurement if one is available.
- Measure the journal OD and the trunnion bore on the actual parts, and confirm the interference lies in the band.
- Confirm the joint model against the actual barrel — groove or hole — and, if a groove, fix its axial position and measure the chamber bore there.
- Build the barrel up in the documented order, with the gas port light check performed and photographed before each pin goes in.
- Press the barrel in incrementally, gauging headspace between increments, until GO closes and NO-GO does not.
- Establish both axes on the mill, lay out, punch, and verify the quadrant before cutting.
- Spot, drill, ream, deburr, and verify the hole with pin gauges.
- Press the pin. Re-verify headspace.
- Function-check, and only then consider anything beyond it.
Steps 1 to 3 are desk-and-bench work with no irreversible operation in them, and they are the entire distance between this build’s current state and being able to start.
24.4 How to Read These Eight Volumes
They are a record of one build’s specifications and reasoning, assembled from the builder’s own notes and calculations, checked where checking was possible, and corrected in three places where the source documents contradicted themselves or each other:
- The through-hole joint description, which the geometry rules out — Vol 23.
- The bearing table computed against generic-steel yield while the analysis’s own commentary used barrel-steel yield — Vol 23.
- The ball end mill speed originally specified above the band the surface-speed arithmetic supports, corrected in a later verification pass — Vol 19.
Those corrections are the most useful content in the build arm, and they exist because the figures were re-derived rather than copied. The same posture applies to everything here: the numbers in these volumes are a starting point for measurement on the parts in front of the reader, not a substitute for it. A dimension taken from a document and cut into a barrel is a dimension nobody has checked.
Sources
- The builder’s project notes, build reference and engineering analysis for this rifle, throughout.
- Vols 17 to 23 of this dive for the derivations summarised here.
Comments (0)